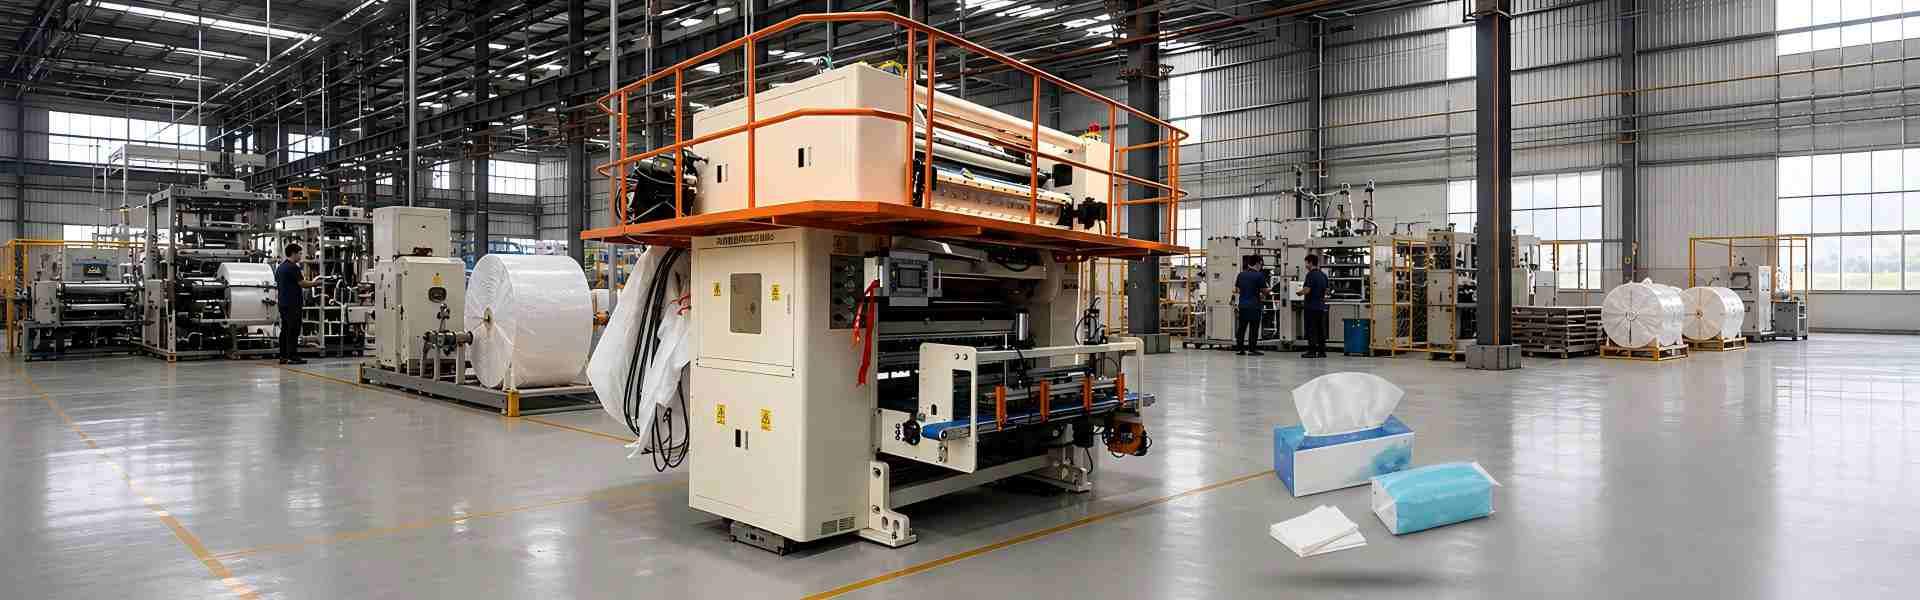
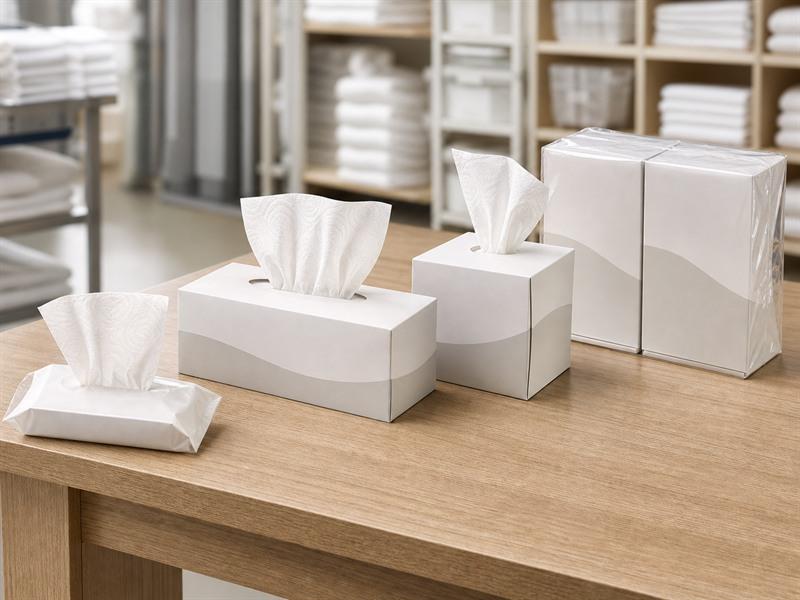
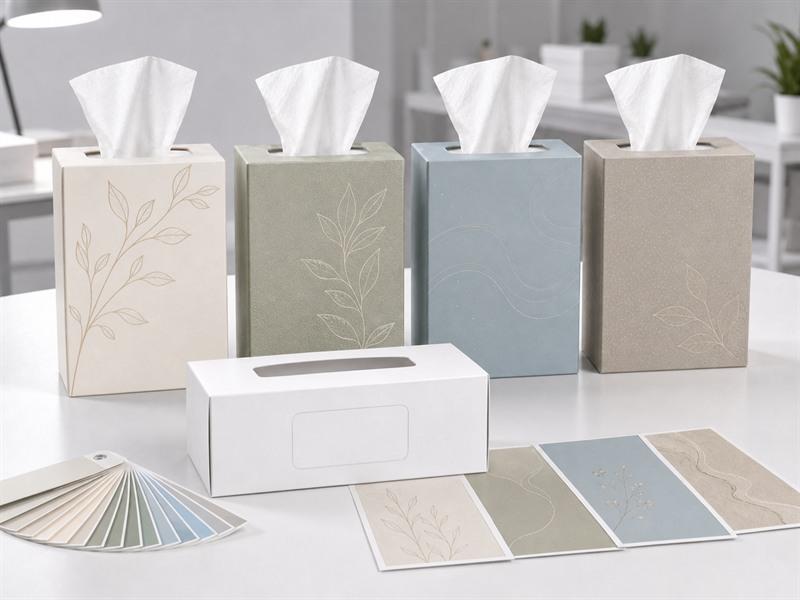
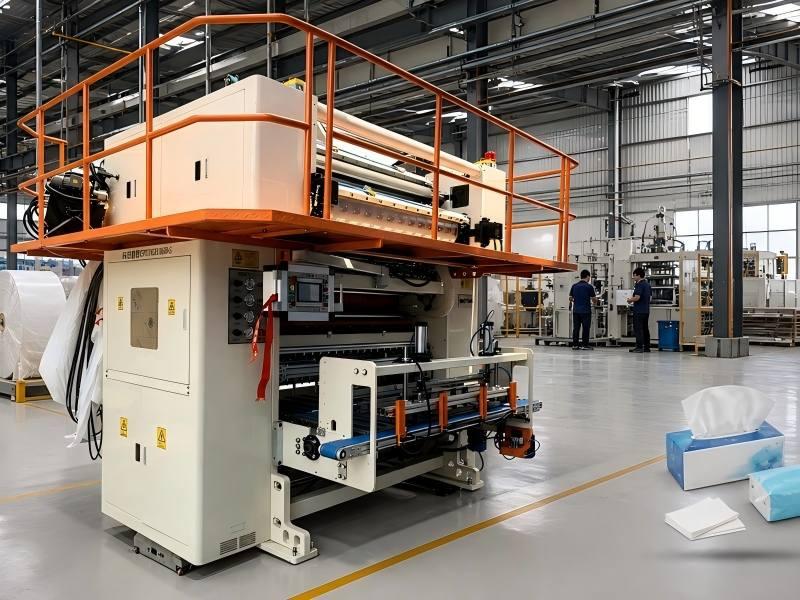
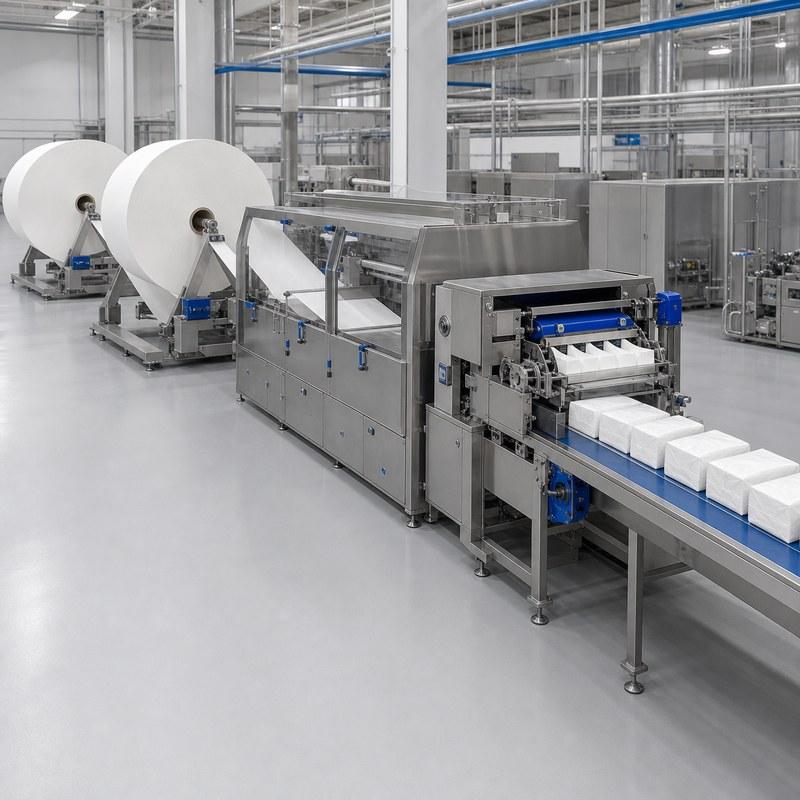
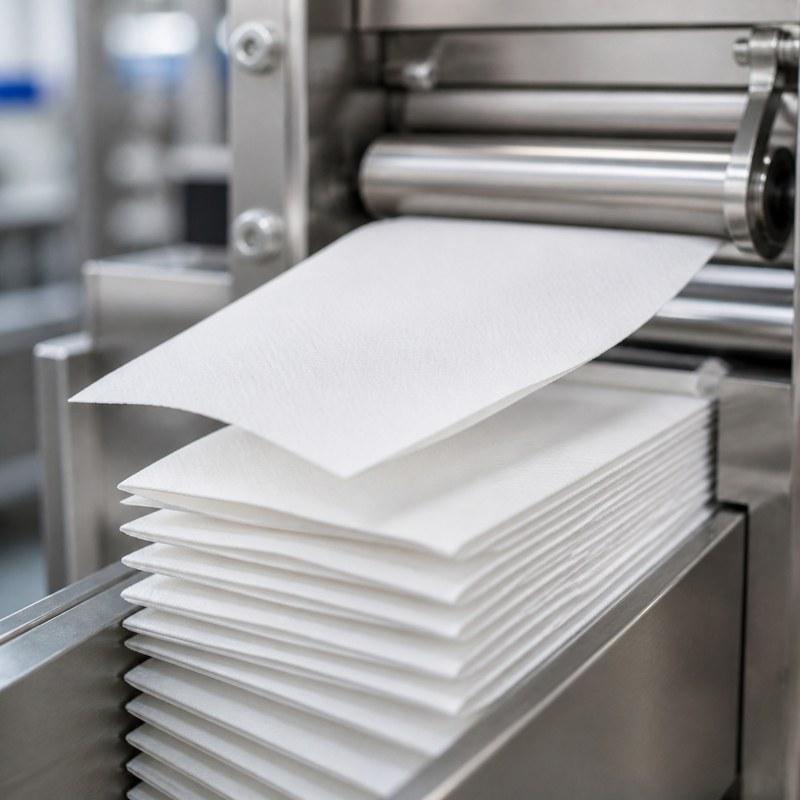
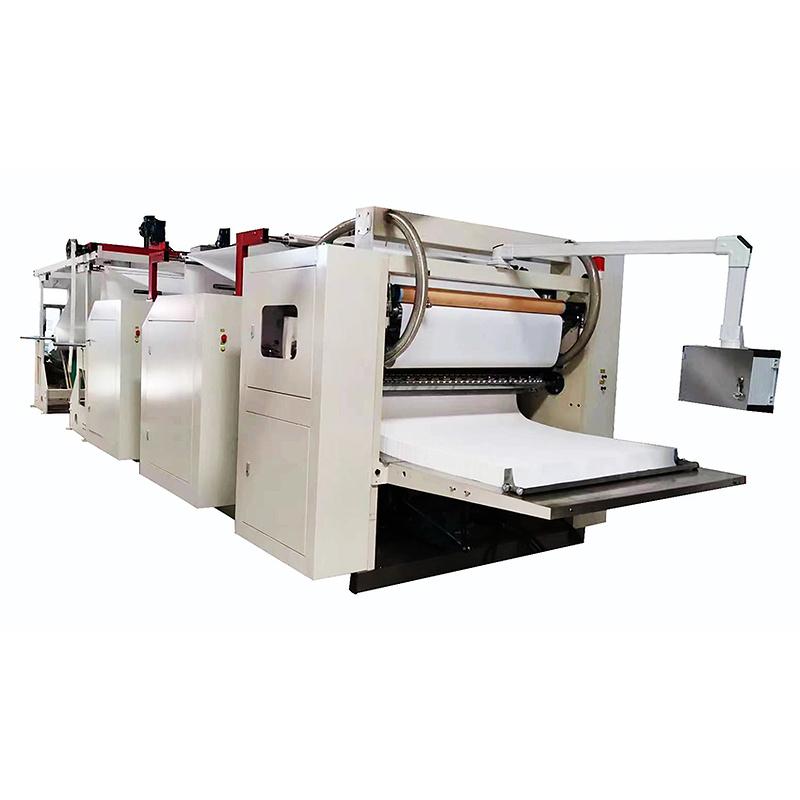
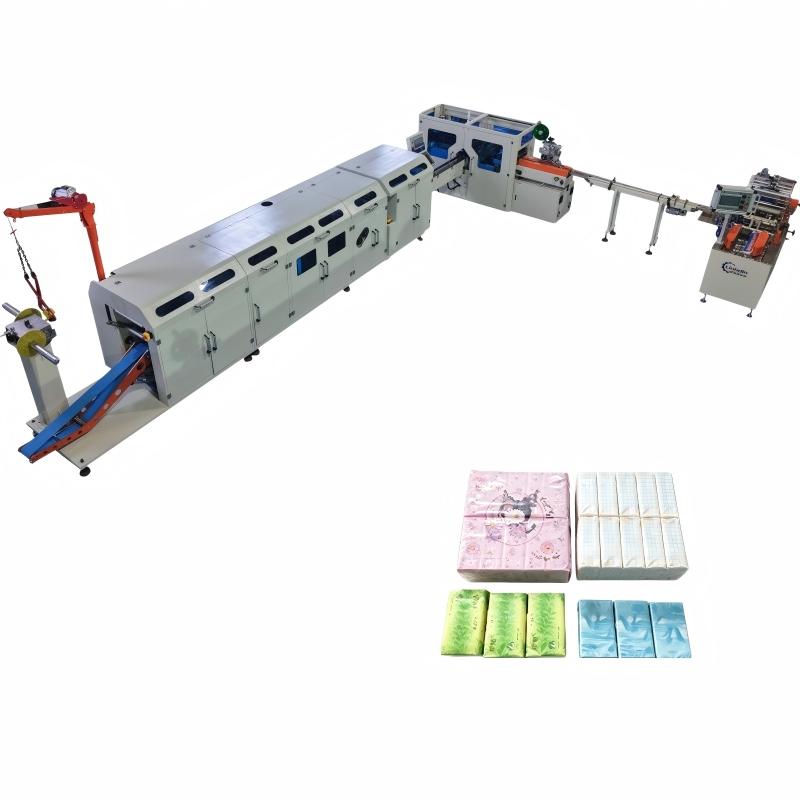
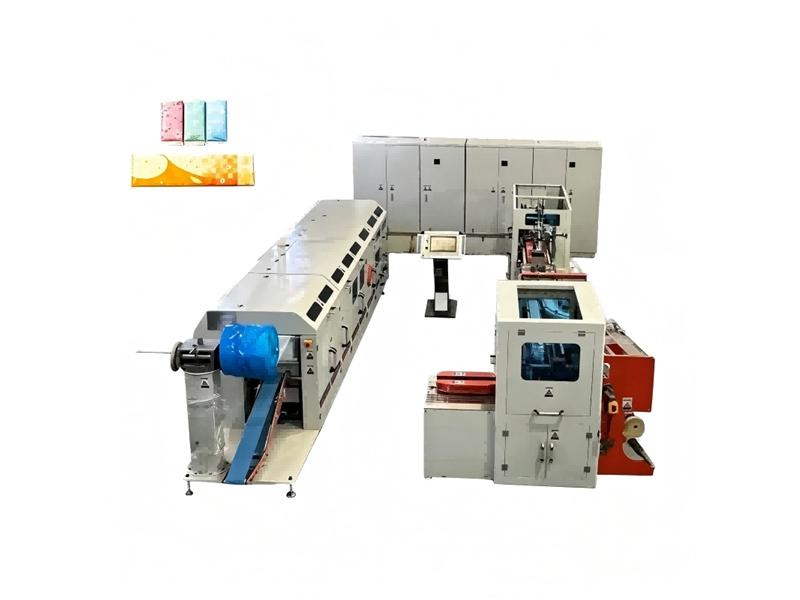
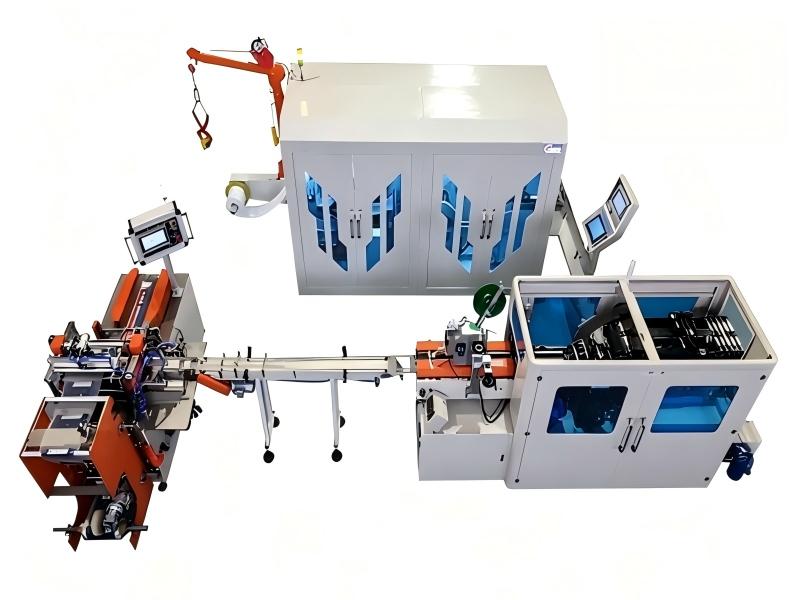
This facial tissue production solution coordinates converting, interfolding, cutting, and packaging for soft-pack and box facial tissue manufacturers. The line manages the process from jumbo roll unwinding through interfolding, log cutting, and final packaging, supporting consistent output of clean, soft, and neatly presented facial tissues for retail and away-from-home markets.
Configuration Decisions
Before finalizing the line, the buyer must confirm the following specifications:
|
Decision Point
|
Options
|
Impact
|
|
Fold type
|
V-fold / interfolding
|
Determines sheet dispensing behavior and consumer experience
|
|
Pack format
|
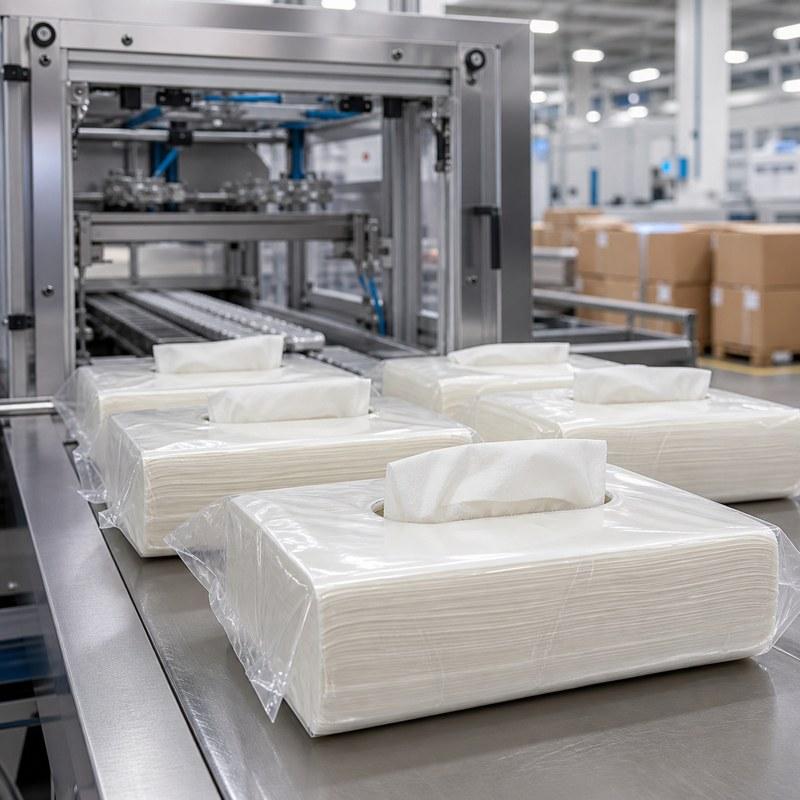
Soft-pack, bottom-pull, bundle, boxed, cube-box
|
Selects the packaging module and transfer interface
|
|
Secondary packaging
|
Shrink-pack (DB-S-550 / DB-S-5525)
|
Adds promotional multi-pack capability after primary packing
|
|
Automation level
|
Manual transfer vs. automatic transfer (DB-T-70)
|
Affects labor requirement and line synchronization
|
Final configuration depends on the finished tissue format, parent-roll specification, target output, packaging requirement, factory layout, and available utilities. These parameters must be confirmed before equipment selection.
Layout & Integration
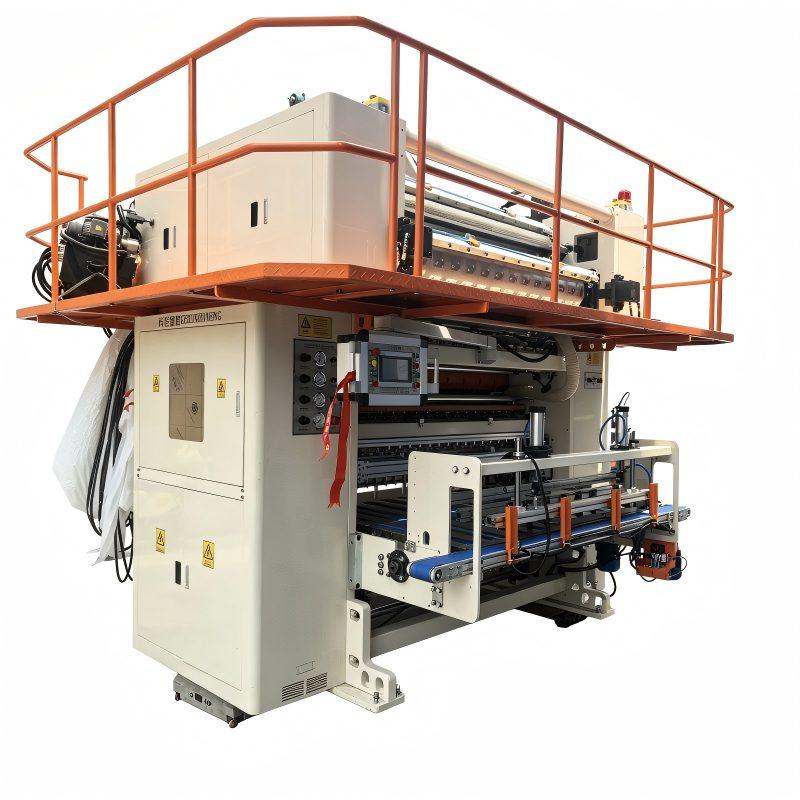
The line is designed for continuous flow from jumbo reel input to finished pack output. Upstream, the DB-FQB800 slitting rewinder must be positioned to feed the interfolder without excessive web tension variation. Downstream, the transfer unit and packaging modules should be arranged to minimize manual handling between cutting and packing. Floor space requirements depend on the selected packaging modules and whether secondary shrink-pack equipment is included. Power supply and compressed air availability must be checked against the combined requirements of the converting and packaging sections.
Quality & Acceptance
Acceptance checks should focus on the finished pack and its dispensing behavior:
-
Verify interfold consistency – each sheet should present the next sheet cleanly during consumer pull.
-
Check log cutting accuracy – pack-length units must be uniform and free of ragged edges.
-
Confirm pack count and seal integrity on the soft-pack or boxed output.
-
Run a line-matching test to confirm transfer speed aligns with both cutting output and packaging speed.
Sample production runs with the actual parent-roll specification and target pack format are required before final acceptance.
Project Input Checklist
For engineering review and configuration recommendation, provide the following:
-
Finished tissue format: soft-pack, bottom-pull, bundle, boxed, or cube-box
-
Sheet size, ply, and fold type (V-fold / interfold)
-
Parent-roll width, diameter, and core size
-
Target output per minute or per shift
-
Pack count per pack and packs per carton
-
Secondary packaging requirement (shrink-pack or bundle)
-
Factory floor plan and available space
-
Power supply standard and voltage
-
Compressed air availability and pressure
To receive a configuration review for your facial tissue line, send your finished product specification, parent-roll details, target output, and packaging requirements. The engineering team will confirm which converting and packaging modules match your production plan.

 Parent Roll / Working Width
 Power Supply / Installed Power
 Tel: +86 139 0819 6540
 Email: info@doubletissuemachine.com
 MP/WhatsApp: +86 139 0819 6540
 Manufacturer Address:Dongguan, Guangdong, China