DB-HK-220P Full Servo Dual-Channel Handkerchief Tissue Production Line
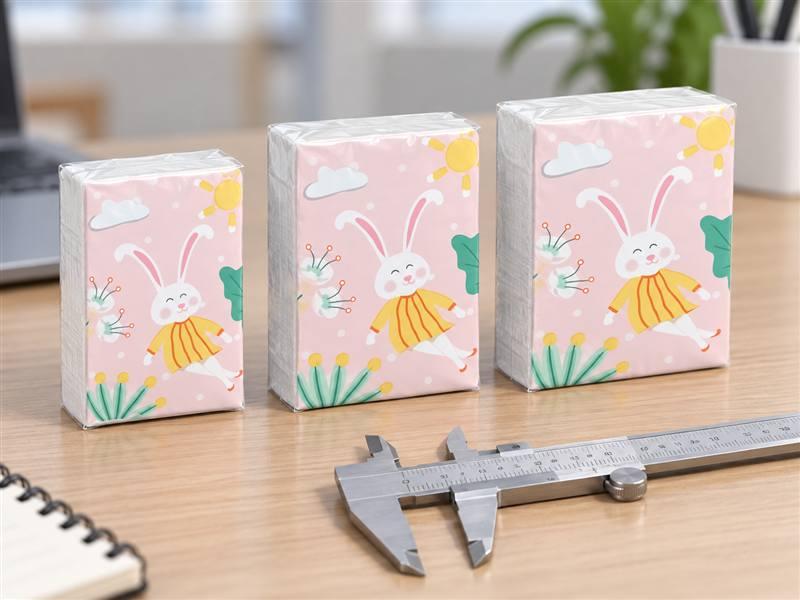
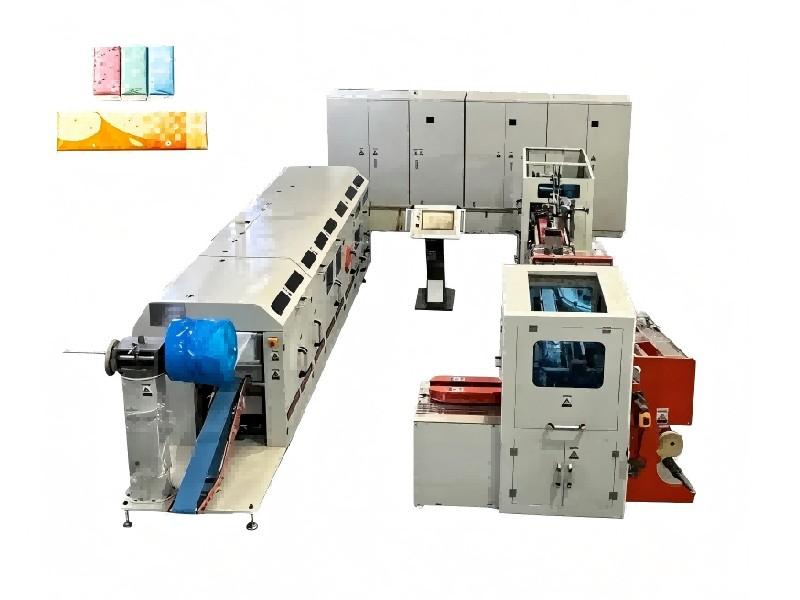
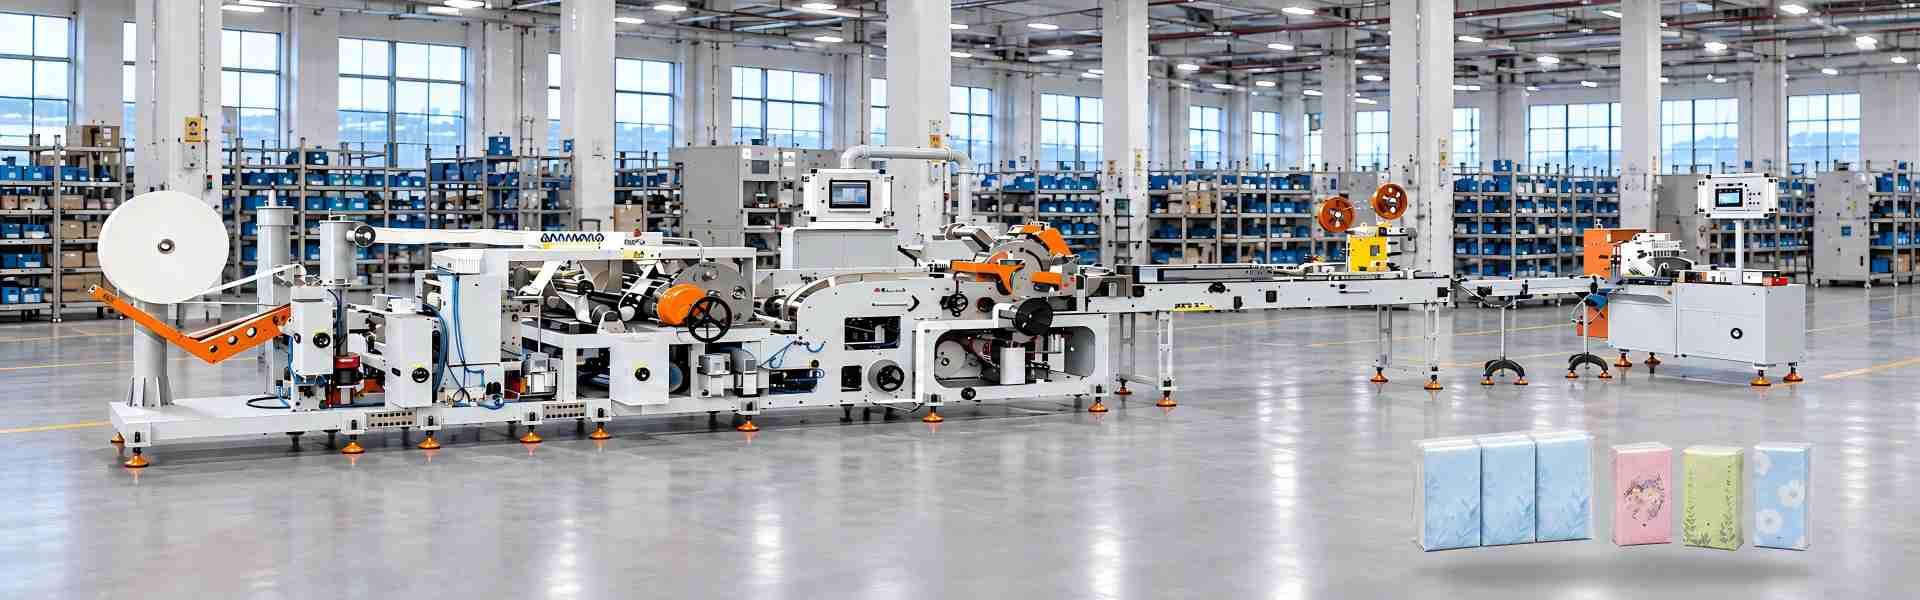
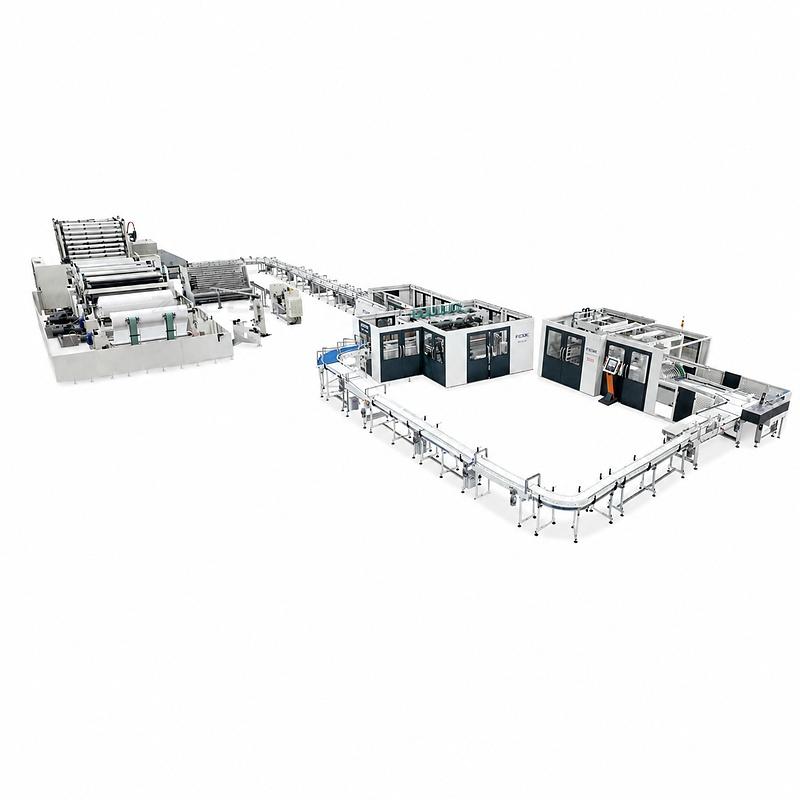
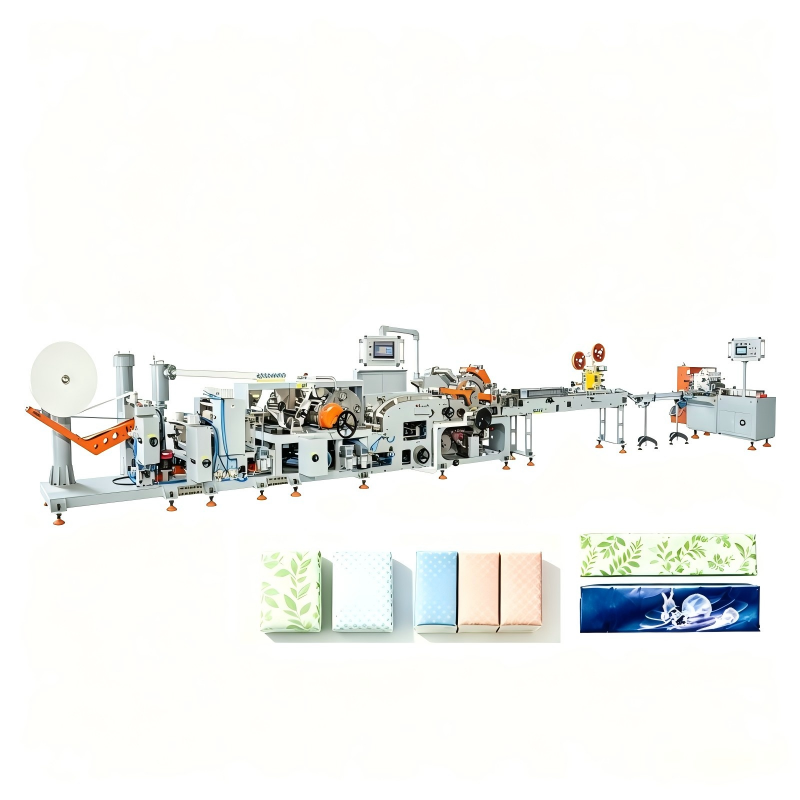
The DB-HK-220P is built for converters who need to run super mini, mini, and standard handkerchief tissue packs on one platform. Its U-shaped dual-channel layout combines full-servo control, constant-tension unwinding, and automatic web correction, so both channels stay synchronized while tissue layers remain aligned through folding and cutting. Rated output is 180–220 packs/min; actual stable output depends on tissue format, base paper quality, and pack specifications, and should be confirmed against your own sample run.
Configuration Choices That Shape Line Performance
-
Base paper: supports 2-ply, 3-ply, and 4-ply tissue, so the same line can serve different market grades.
-
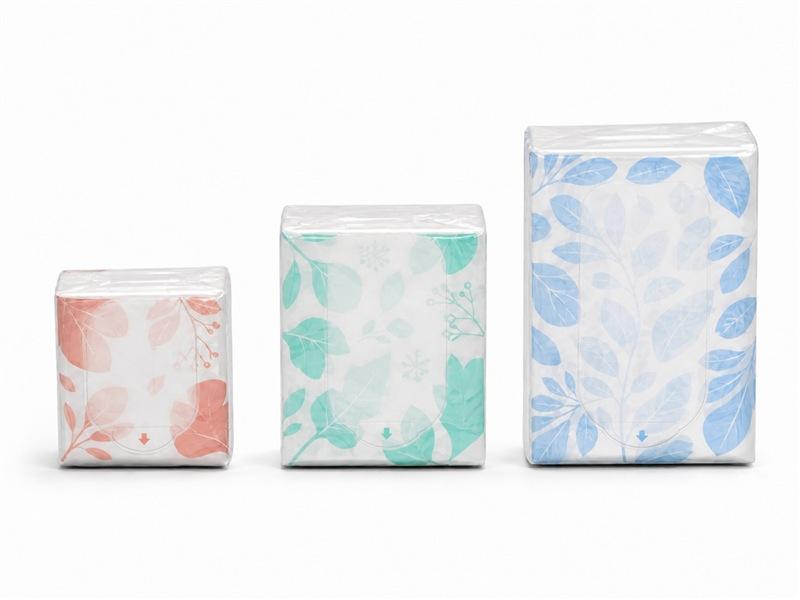
Pack format: super mini, mini, and standard packs with adjustable sheet counts per pack.
-
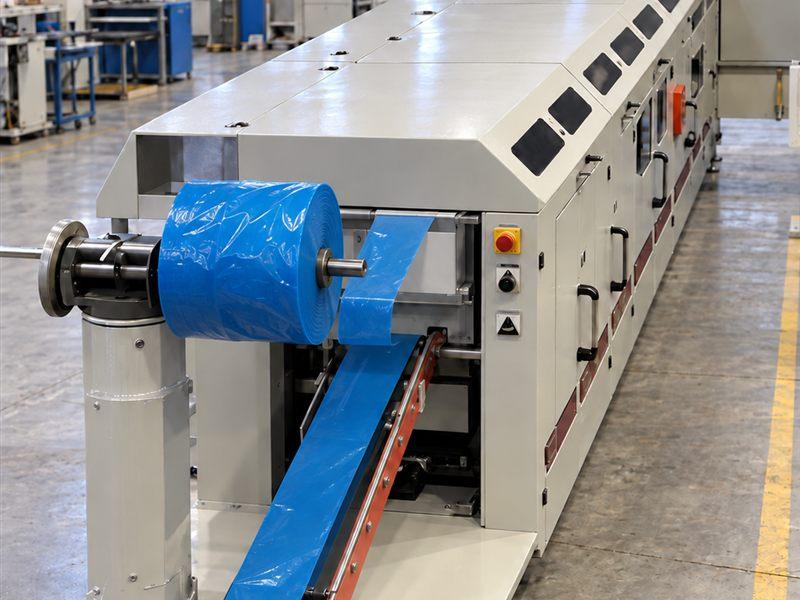
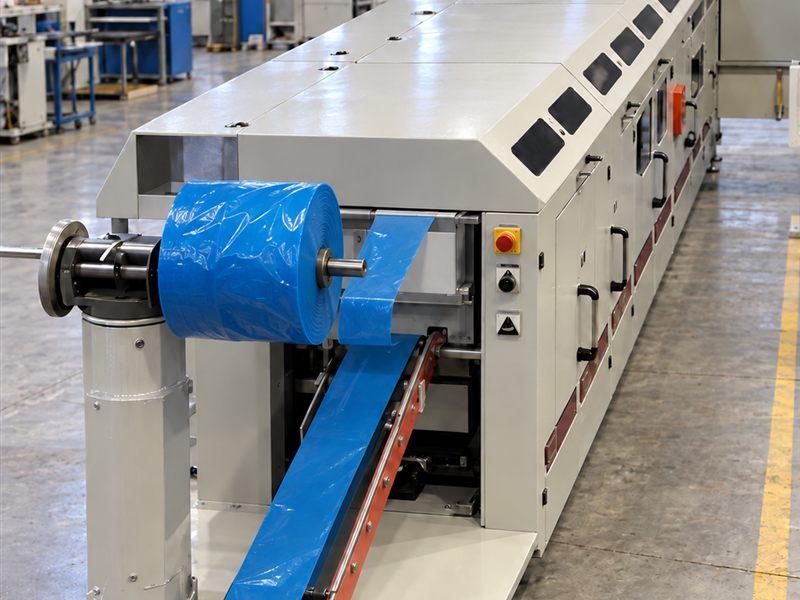
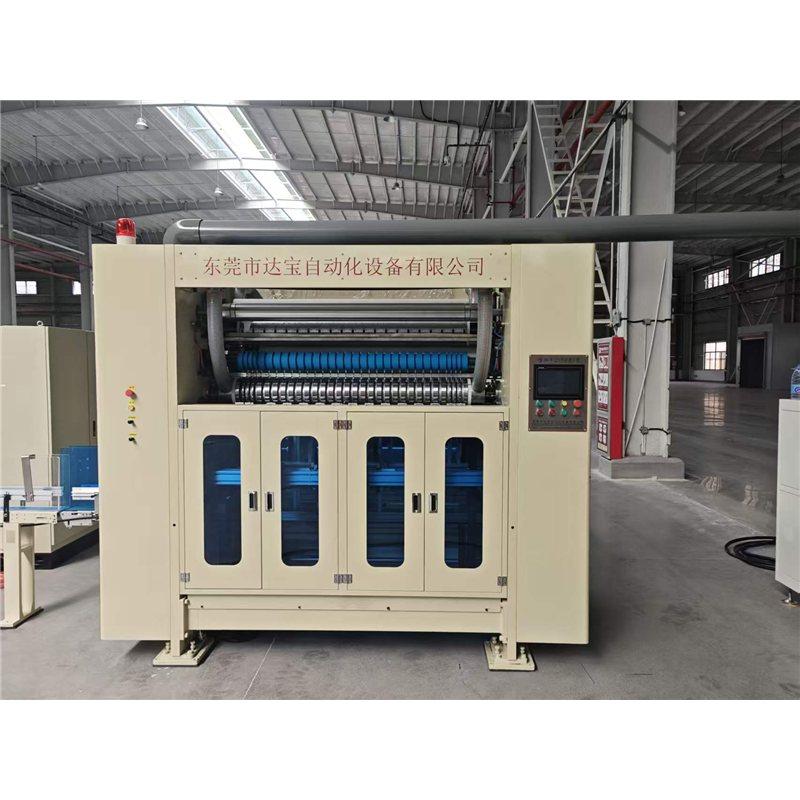
Web handling: servo constant-tension unwinding and automatic web correction help keep tissue layers aligned and reduce manual re-threading.
-
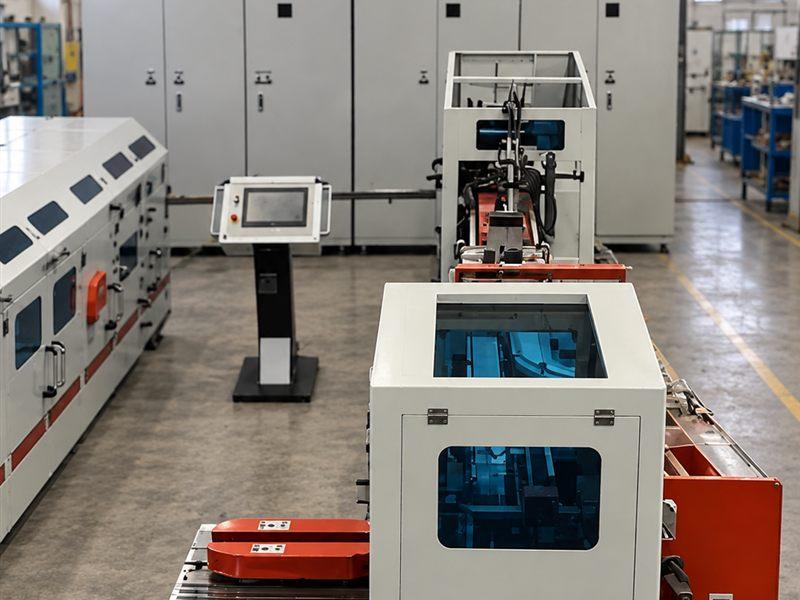
Control: PLC touchscreen HMI covers operation, parameter adjustment, and recipe storage for repeatable changeovers.
-
Output structure: dual-channel production supports high-volume output when both channels run the same format.
Optional Modules And Downstream Integration
Embossing, perforation, automatic labeling, and a multi-language HMI can be configured as required. Connection to bundling or secondary packing equipment can be discussed according to the final production layout. Because these choices affect line length, utilities, and operator access, they should be fixed before the layout is finalized rather than after installation.
What To Prepare Before A Line Proposal
To quote accurately, the factory needs your finished pack format and sheet count, base paper ply and jumbo roll width, target stable output, available floor space, local voltage, and compressed air supply. If any of these are still open, mark them as to be confirmed so the proposal reflects a realistic configuration instead of an assumed one.
|
Project Input
|
Why It Matters
|
|
Finished pack format and sheet count
|
Determines folding, cutting, and counting setup across both channels.
|
|
Base paper ply and jumbo roll width
|
Affects unwinding tension settings and web correction behavior.
|
|
Target stable output
|
Confirms whether the required rate is achievable for your tissue grade.
|
|
Floor space and line layout
|
Sets the U-shaped channel arrangement and downstream access.
|
|
Local voltage and compressed air supply
|
Needed for utility connection planning and commissioning.
|
Operating And Maintenance Notes
During commissioning, verify web tension on both channels before raising speed, and check that automatic web correction is tracking correctly at the folding section. Recipe storage in the HMI shortens changeover between pack formats, but operators should still confirm sheet count and fold alignment on the first packs of each run. Keep the unwinding and folding areas clear for maintenance access, and plan spare wear parts based on your actual running hours rather than a fixed schedule.
Buyer Questions
-
Can one line run super mini, mini, and standard packs?
-
Yes, the DB-HK-220P is designed for these three handkerchief pack formats with adjustable sheet counts. Changeover settings should be confirmed for your specific pack sizes.
-
What determines the achievable output?
-
Base paper quality, ply, pack format, and sheet count all influence stable output. The rated range is a design reference; your acceptance value should be agreed against sample production.
-
Can the line connect to downstream packing?
-
Connection to bundling or secondary packing equipment can be discussed according to the final production layout. Interface details depend on the selected downstream machine.

 Line Layout Size
 Line Weight

 Tel: +86 139 0819 6540
 Email: info@doubletissuemachine.com
 MP/WhatsApp: +86 139 0819 6540
 Manufacturer Address:Dongguan, Guangdong, China


0 reviews